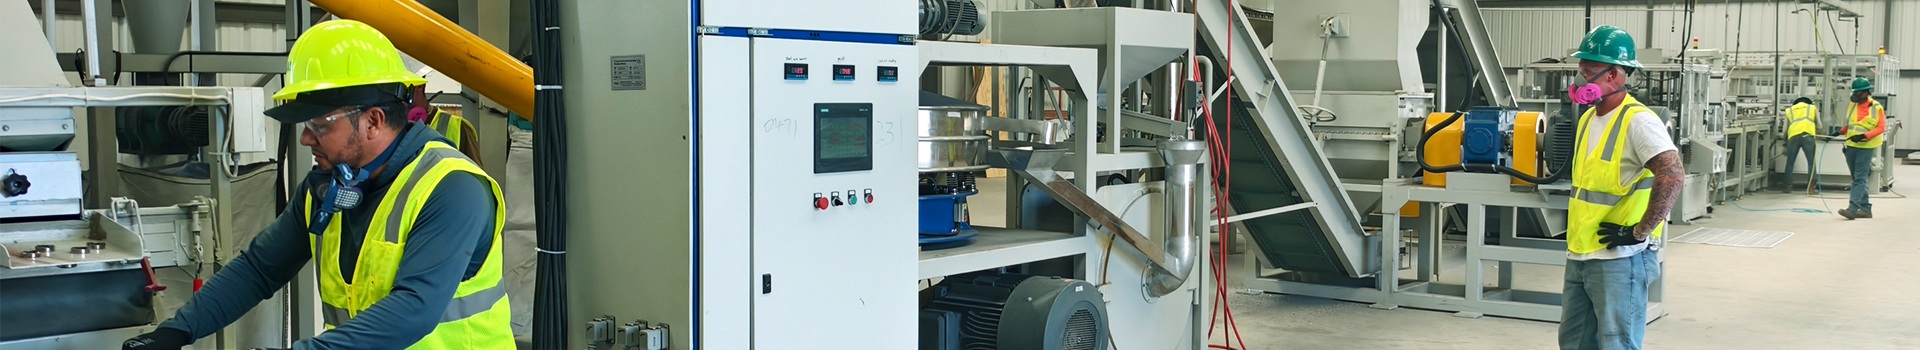
Investing in a Lithium Battery Recycling Plant
The global transition toward electric mobility and renewable energy storage has unleashed an unprecedented volume of end-of-life batteries. For waste management companies, metal smelters, and sustainability ventures, investing in a commercial lithium battery recycling plant is no longer just a regulatory compliance measure—it is one of the highest-margin industrial recycling opportunities today.
The primary financial driver of battery scrap processing lies in the extraction of black mass, the cathode-anode powder rich in nickel, cobalt, manganese, and lithium. However, the profitability of this process depends on metallurgical purity: downstream hydrometallurgical refiners pay steep premiums for black mass with negligible copper and aluminum contamination.
Henan Recycle addresses this bottleneck with continuous mechanical separation systems engineered to achieve industry-leading recovery metrics at processing capacities of 800 to 1,000 kg/h:
Black Mass: Recovery rate > 97%, purity > 98% (copper contamination < 2%, aluminum contamination < 1%)
Copper Granules: Recovery rate > 95%, product purity > 95%
Aluminum Fractions: Recovery rate > 88%, purity > 82%
Diaphragm Film (Separator): Recovery rate > 95% with 97% purity
Operating via an advanced physical-mechanical route—integrating safe shredding, multi-stage crushing, magnetic separation, dynamic air classification, and gravity shaking tables—the line avoids the heavy operational expenses and wastewater treatment burdens associated with direct chemical pre-treatment.
By converting mixed cylindrical cells, pouch packs, and prismatic modules into distinct, market-ready commodities (steel shells, pure copper, aluminum flakes, and premium black mass), processors capture immediate value at both ends of the supply chain.
Discover turnkey configurations and request a quote for your facility:
> Explore the Henan Recycle Lithium Battery Recycling Plant